Food Grade Bucket Elevator Manufacturer
Product Profile
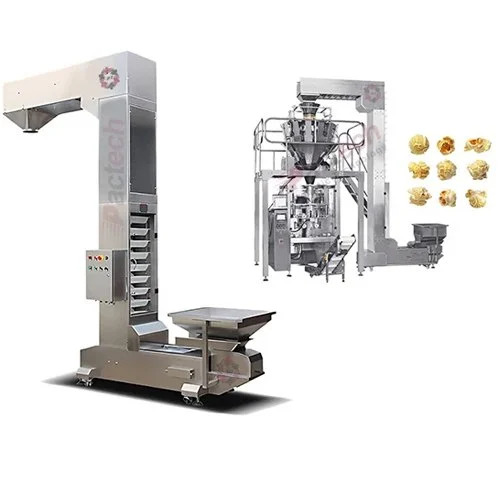
Annovaa Industries Pvt. Ltd. is a manufacturer of Food Grade Bucket Elevators for food-processing and grain-handling industries in Kolkata, West Bengal, Jharkhand, Odisha, Assam and Chhattisgarh. Designed for controlled vertical movement of bulk materials, these elevators provide an efficient way to transfer grains, cereals, pulses and other food-grade products between different processing levels while reducing unnecessary manual handling.
Vertical Material Handling for Food Processing Plants
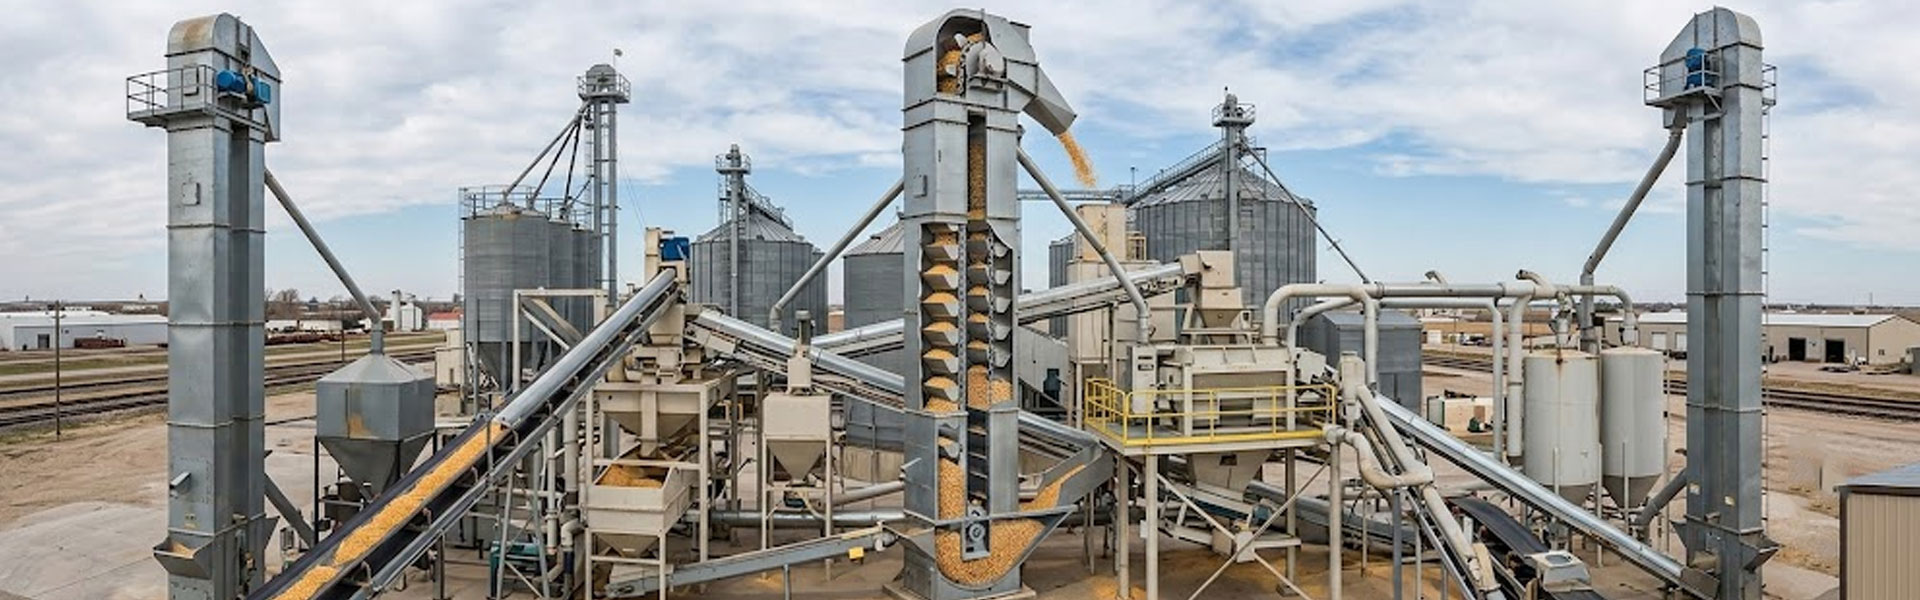
A Food Grade Bucket Elevator is a vertical conveying system that uses a series of buckets attached to a continuously moving belt or chain. The buckets collect material from the lower section, carry it upward and discharge it at the required elevation. Unlike ordinary material-handling elevators, food-grade equipment requires greater attention to hygiene, product-contact surfaces, accessibility and contamination control. The machine can therefore be configured according to the requirements of the food-processing environment.
From Receiving Area to Processing Line
Bucket elevators are particularly useful when a production plant has limited floor space but requires material to move between different levels.
A typical conveying cycle includes:
Feeding → Bucket Filling → Vertical Lifting → Controlled Discharge → Transfer to Next Stage
The elevator can be incorporated into a larger grain or food-processing line, allowing materials to move continuously between cleaning, grading, milling, storage or packing sections.
Food-Grade Construction Features
Annovaa Industries Pvt. Ltd. focuses on construction details that are important when the conveyed material is intended for food-processing applications.
Key considerations include:
- Smooth product-contact surfaces
- Hygienic internal construction
- Suitable food-processing-grade components
- Properly finished bucket surfaces
- Reduced material retention areas
- Accessible inspection sections
- Enclosed conveying arrangement
- Easy cleaning and maintenance access
- Robust supporting structure
The final construction can be selected according to the material being handled and the hygiene requirements of the installation.
What Can Be Conveyed?
Food Grade Bucket Elevators can be used for vertical handling of a variety of dry bulk food materials, depending on the bucket design and machine configuration.
Common materials include:
- Rice and paddy
- Wheat
- Maize
- Pulses
- Cereals
- Seeds
- Grains
- Flour and selected dry food powders
- Processed food ingredients
- Other free-flowing bulk materials
The appropriate bucket shape, capacity and conveying speed should be selected according to the characteristics of the product.
Engineering Details That Matter
The performance of a bucket elevator depends on several interconnected components rather than the buckets alone. Annovaa Industries Pvt. Ltd. considers the complete conveying arrangement while supplying equipment.
Important elements include:
- Elevator Buckets
Buckets are selected according to the material characteristics, required capacity and discharge arrangement.
- Belt or Chain System
The continuous lifting mechanism transfers the buckets through the vertical casing.
- Drive Assembly
The motor and drive arrangement provides the required movement for continuous material lifting.
- Head and Boot Sections
These sections manage loading, elevation and discharge of the conveyed material.
- Casing
The enclosed casing guides the buckets and helps maintain an organized vertical conveying path.
- Inspection Arrangements
Suitable access points allow operators to inspect and maintain important internal components.
Technical Specification Guide
Parameter | Typical Configuration |
Product | Food Grade Bucket Elevator |
Conveying Direction | Vertical |
Application | Food & Grain Material Handling |
Conveyed Material | Dry Bulk Food Products |
Bucket Arrangement | Continuous Bucket Series |
Drive | Motor Driven |
Casing | Enclosed Industrial Construction |
Feeding | Continuous or Controlled Feeding |
Discharge | Top Discharge Arrangement |
Installation | Processing Plant / Material Handling Line |
Capacity | Based on Product & Plant Requirement |
Elevator Height | According to Site Requirement |
Exact bucket capacity, belt/chain arrangement, motor rating, elevator height and construction materials can be finalized according to the customer’s application.
Benefits for Food-Processing Operations
- Better Use of Vertical Space
The elevator allows materials to travel upward without requiring a long horizontal conveyor route.
- Continuous Material Transfer
It can support uninterrupted movement between different stages of a processing line.
- Reduced Manual Handling
Automated vertical conveying reduces the need for repeated lifting and transferring of bulk materials.
- Controlled Product Movement
A properly designed bucket arrangement helps maintain a steady material flow.
- Enclosed Conveying
The enclosed design can help protect the conveyed product from unnecessary exposure during transfer.
- Flexible Plant Integration
The elevator can be incorporated into grain cleaning, milling, storage and packaging systems.
Applications across Food and Grain Industries
Food Grade Bucket Elevators from Annovaa Industries Pvt. Ltd. can be considered for:
- Rice mills
- Flour mills
- Pulse processing plants
- Grain cleaning facilities
- Cereal processing units
- Seed-processing plants
- Food ingredient facilities
- Bulk food handling systems
- Agricultural processing industries
- Storage and transfer sections
Manufacturing & Quality Approach
At Annovaa Industries Pvt. Ltd., manufacturing begins with understanding the required lifting height, material characteristics, and throughput and plant layout. Structural parts are fabricated with attention to dimensional accuracy, while the bucket arrangement, drive system and casing are assembled for smooth material movement.
Quality checks can cover:
- Structural fabrication
- Bucket alignment
- Drive assembly
- Shaft and bearing arrangement
- Casing fitment
- Surface finishing
- Fastener and component installation
- Trial inspection before dispatch
For food-processing applications, particular attention is given to areas that come into contact with the conveyed material.
Designed Around Your Plant Layout
Every processing facility has different floor levels, feeding points and discharge locations. Therefore, a bucket elevator should be selected according to the complete material-handling route.
Annovaa Industries Pvt. Ltd. can help determine suitable configurations based on:
- Required lifting height
- Material type
- Required conveying capacity
- Feeding arrangement
- Discharge point
- Available installation space
- Existing machinery
- Cleaning and maintenance requirements
Why Choose Annovaa Industries Pvt. Ltd.?
Annovaa Industries Pvt. Ltd. supplies food and grain-processing machinery for customers across Kolkata, West Bengal, Jharkhand, Odisha, Assam and Chhattisgarh.
Customers can approach us for:
- Food Grade Bucket Elevator requirements
- New plant installations
- Machinery replacement
- Processing-line integration
- Customized dimensions
- Bulk-order requirements
- Technical product guidance
- Competitive commercial solutions
Get a Food Grade Bucket Elevator for Your Processing Plant
If your facility requires dependable vertical movement of grains, cereals, pulses or other dry food materials, Annovaa Industries Pvt. Ltd. can provide a Food Grade Bucket Elevator configured around your processing requirements. Contact Annovaa Industries Pvt. Ltd. for Food Grade Bucket Elevator specifications, capacity, dimensions, installation requirements and pricing in Kolkata, West Bengal, Jharkhand, Odisha, Assam and Chhattisgarh.