Silo Bin Activator Manufacturer
Reliable Discharge Solutions for Industrial Storage Silos
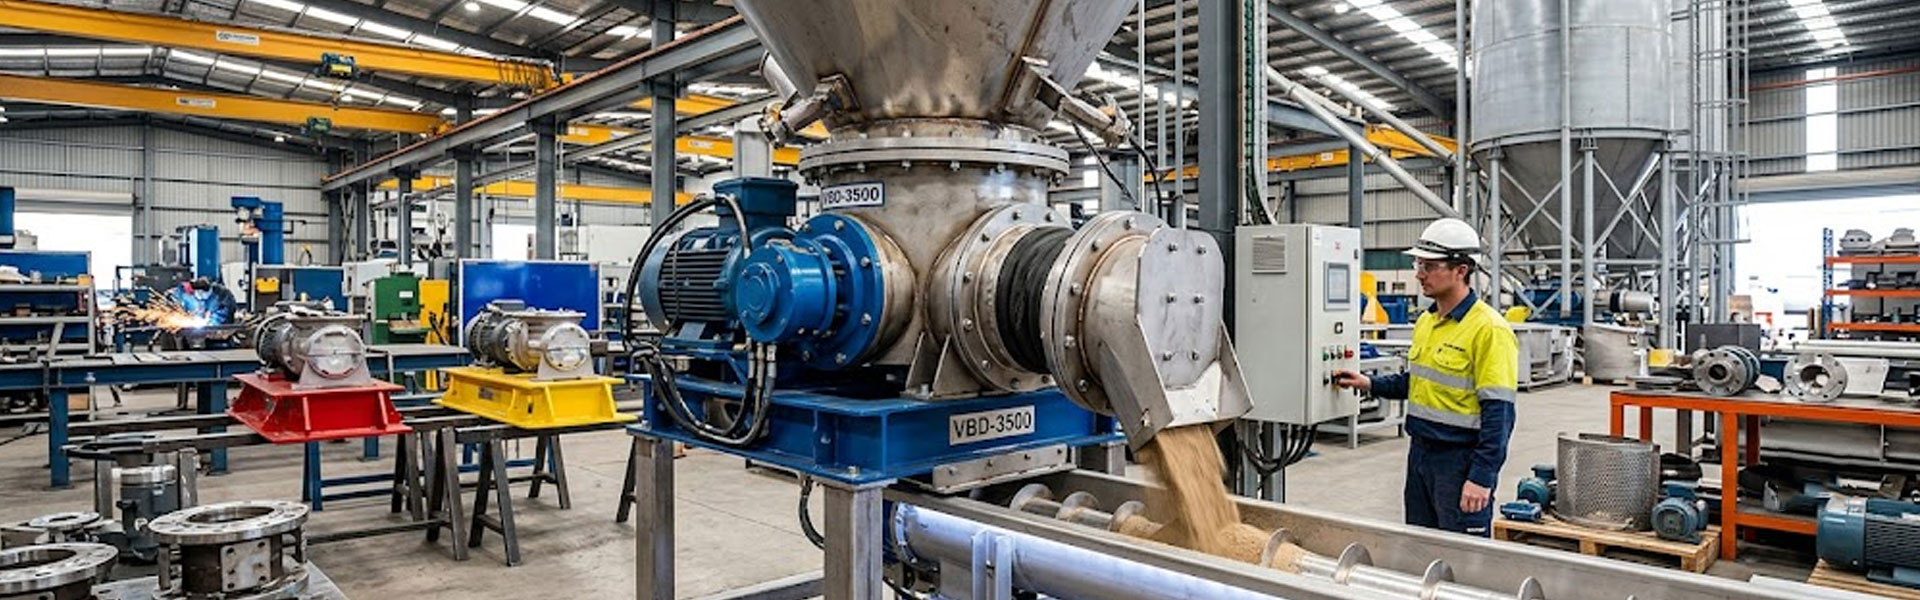
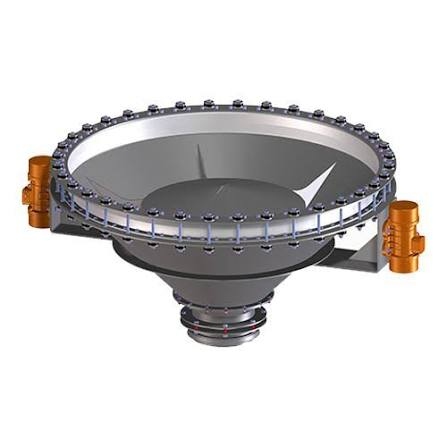
Annovaa Industries Pvt. Ltd., a trusted Silo Bin Activator Manufacturer, offers reliable solutions for industrial facilities that need dependable emptying of bulk materials stored in silos, hoppers, and large storage vessels. During storage, certain powders and granular materials may compact, form arches, or stick to internal surfaces, preventing them from moving freely toward the outlet. A bin activator helps address these flow difficulties by creating controlled movement around the discharge zone.
Designed for integration with bulk-material handling systems, our silo bin activators support operations in flour mills, grain processing plants, chemical units, fertilizer facilities, and other manufacturing environments. Businesses across Kolkata, West Bengal, Jharkhand, Odisha, Assam, and Chhattisgarh can explore custom configurations based on their storage structure, material properties, and discharge requirements.
How Does a Silo Bin Activator Work?
A silo bin activator is generally fitted beneath the conical or hopper-shaped section of a storage silo. Its drive mechanism generates controlled vibration or movement in the activator assembly, helping material travel toward the outlet instead of remaining stagnant along the walls. The system is selected according to factors such as material density, moisture content, particle size, silo geometry and the required discharge rate. When correctly matched to the application, it can improve material withdrawal and support a more consistent supply to downstream equipment.
Operational Features That Support Bulk Handling
- Assisted material movement:Helps loosen material near the silo outlet and encourages discharge.
- Reduced flow obstruction:Can help limit bridging and ratholing problems when appropriately engineered for the material.
- Silo-bottom integration:Designed to connect with suitable hopper or silo outlet arrangements.
- Process continuity:Supports material transfer to screw conveyors, belt conveyors, mixers and feeding equipment.
- Application-based construction:Contact surfaces and structural materials can be selected to suit operating conditions.
- Adaptable installation:Configuration can be planned around silo geometry, available space and the connected process line.
- Controlled operation:Drive and control arrangements can be selected to match the plant’s operating sequence.
Advantages for Storage and Production Facilities
- More Effective Silo Emptying
The activator helps mobilize material around the discharge region, reducing the likelihood of product remaining trapped near the outlet.
- Improved Downstream Supply
A more consistent discharge can help connected machines receive material with fewer interruptions caused by storage-flow issues.
- Less Dependence on Manual Clearing
When correctly specified, the system can reduce the need for frequent manual intervention to restore material flow.
- Better Use of Storage Capacity
By assisting material movement toward the outlet, a suitable activator can help reduce inactive material zones within the discharge area.
- Support for Continuous Processing
Industries that transfer stored ingredients or raw materials into production equipment can use the system as part of a coordinated material-handling arrangement.
Industries That Use Silo Bin Activators
Annovaa Industries Pvt. Ltd.’s Silo Bin Activator solutions can be considered for applications such as:
- Flour and grain mills:Handling wheat, flour, bran and other grain-based materials.
- Food manufacturing:Discharging suitable dry ingredients from storage silos.
- Chemical processing:Moving selected powders and granules into dosing or mixing systems.
- Fertilizer plants:Supporting the handling of compatible bulk fertilizer materials.
- Cement and mineral units:Assisting the discharge of suitable dry raw materials.
- Animal feed production:Transferring grains and feed ingredients to processing equipment.
- Plastic and polymer processing:Handling compatible resin granules and powdered additives.
- Batching and packaging plants:Supplying materials to metering, weighing and packing systems.
Material compatibility, dust-control requirements and hygiene needs should be evaluated before final equipment selection.
Engineered Around Your Silo Configuration
A Silo Bin Activator must work with the storage vessel rather than simply fit beneath it. Annovaa Industries Pvt. Ltd. considers key application details to help customers identify an appropriate arrangement for their facility. Important selection factors include silo outlet diameter, cone angle, bulk density, flow characteristics, material abrasiveness, operating temperature and target discharge rate. The mounting arrangement, drive selection and structural design should also account for the loads and movement generated during operation. For industrial projects in Kolkata and across West Bengal, Jharkhand, Odisha, Assam and Chhattisgarh, these details help establish whether a standard or customized configuration is suitable.
Technical Specifications of Silo Bin Activator
Specification | Available Design Considerations |
Equipment Type | Silo Bin Activator |
Primary Function | Assisting discharge from silos and hoppers |
Installation Location | Beneath a compatible silo or hopper outlet |
Material Compatibility | Selected powders, granules and dry bulk solids |
Activating Mechanism | Vibration-based or application-specific drive arrangement |
Construction Material | Mild steel, stainless steel or other suitable material |
Outlet Connection | Designed to match the silo and downstream equipment |
Capacity | Determined by material characteristics and process demand |
Drive System | Selected according to equipment design and duty cycle |
Control Arrangement | Standalone or integrated plant control, as required |
Sealing and Dust Control | Selected according to product and process requirements |
Custom Design | Based on silo dimensions and operating conditions |
The final design, capacity, dimensions, motor rating and construction details should be confirmed against the actual application. The table describes selection considerations, not guaranteed standard specifications.
Silo Bin Activator for Integrated Material Handling Systems
A Silo Bin Activator can form part of a wider material-handling setup that includes storage silos, rotary valves, screw conveyors, weighing systems and automated feeding equipment. Correct coordination between these components helps avoid bottlenecks between raw-material storage and production. For example, a flour processing plant may use a silo bin activator to assist the movement of stored grain or flour into a conveyor feeding the next operation. In a powder-handling facility, the arrangement may be selected to supply a mixer or dosing unit. Each application requires a design suited to the specific product and process conditions.
Why Consider Annovaa Industries Pvt. Ltd.?
Annovaa Industries Pvt. Ltd. works with industrial machinery requirements where equipment selection needs to reflect the customer’s actual process. For Silo Bin Activator enquiries, customers can discuss:
- The type and properties of the stored material
- Silo dimensions and outlet configuration
- Required discharge capacity
- Compatibility with existing conveyors and feeders
- Construction material and operating environment
- Installation constraints and customization needs
This information helps establish a practical equipment specification for commercial and industrial projects.
Request a Quote for a Silo Bin Activator
If you are searching for a Silo Bin Activator Manufacturer in Kolkata, West Bengal, Jharkhand, Odisha, Assam and Chhattisgarh, contact Annovaa Industries Pvt. Ltd. to discuss your plant requirements. Share the material name, silo size, outlet dimensions, required throughput and preferred construction material to help determine a suitable solution. Contact Annovaa Industries Pvt. Ltd. for product details, customized equipment enquiries and bulk-order quotations.